
Our History
Established in 2013, QHY Bioengineering Co., Ltd. is a high-tech manufacturer specializing in peptides and supplements. With a modern 17,000-square-meter production facility, we provide integrated R&D, customization, and manufacturing solutions for customers worldwide.
Our capabilities cover custom peptide synthesis, supplement formulation and development, product customization, and scalable manufacturing. Whether you are developing a new product, refining an existing formula, or preparing for larger-scale production, our team can support you from the early development stage through manufacturing and packaging.
Over the years, we have worked with biotech companies, laboratories, research teams, distributors, and brand owners in both domestic and international markets. Our experience in peptide and supplement manufacturing allows us to provide flexible solutions tailored to different product requirements, specifications, and market needs.
We focus on making product development and manufacturing more straightforward-from initial concept and R&D to small-batch testing and commercial-scale production-while maintaining consistent quality, reliable supply, and responsive support throughout the process.
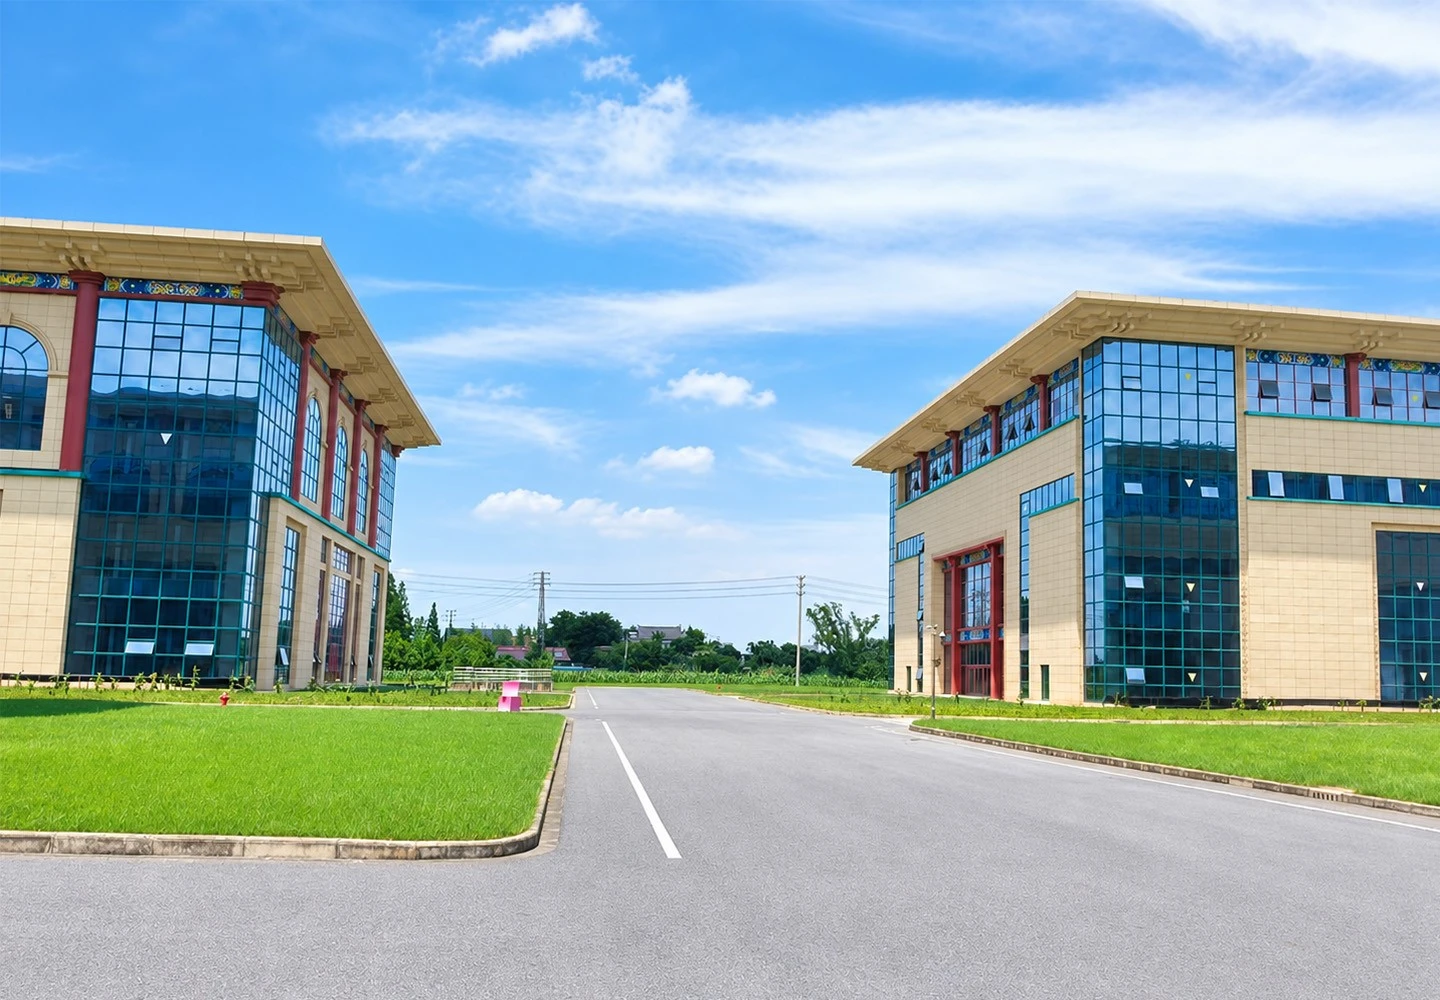
Manufacturing and Quality Advantages
Strict Quality Control (QC)
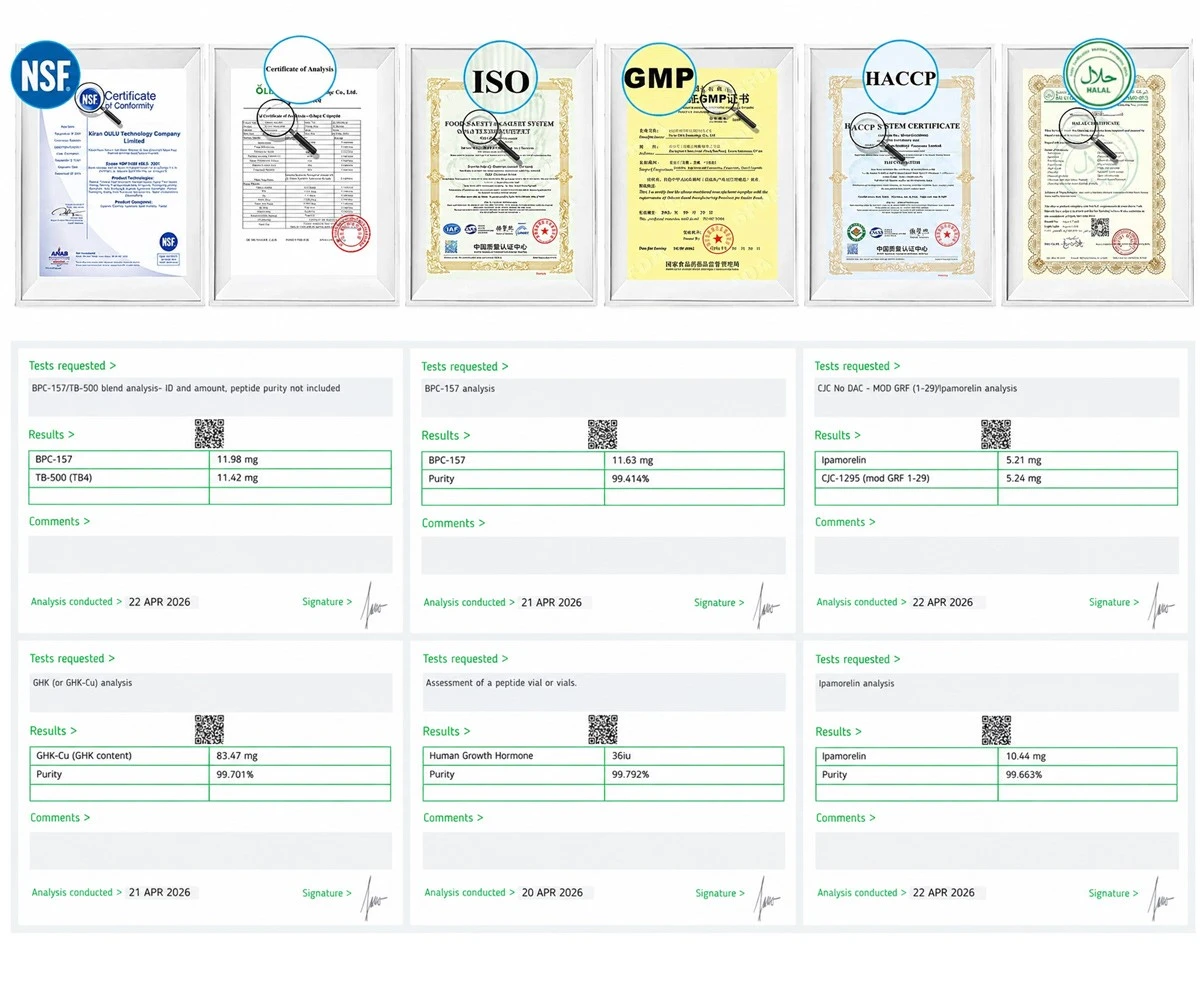
Before every batch leaves our factory, we run two‑step tests with HPLC and MS to double‑check product quality. Our production follows ISO9001 and cGMP‑compliant standards.
Fast Order Delivery
We own our independent production workshops and work with well‑established supply‑chain partners. This lets us deliver orders faster than many suppliers in this industry, so you won't need to worry about long waiting times.
Worldwide Shipping
We have rich practical experience in peptide export, with clients across North America, Europe, Asia and more regions.
All products are professionally packaged to ensure safe, secure, and compliant international shipping.
Our Product
Peptides & Supplement Ingredients
We offer research peptides, custom peptide synthesis, cosmetic peptides, and peptide pharmaceutical intermediates;
Our supplement solutions include **creatine, protein powder, collagen, plant extracts, minerals, and other customized ingredients**, supporting diverse formulation and product development needs.
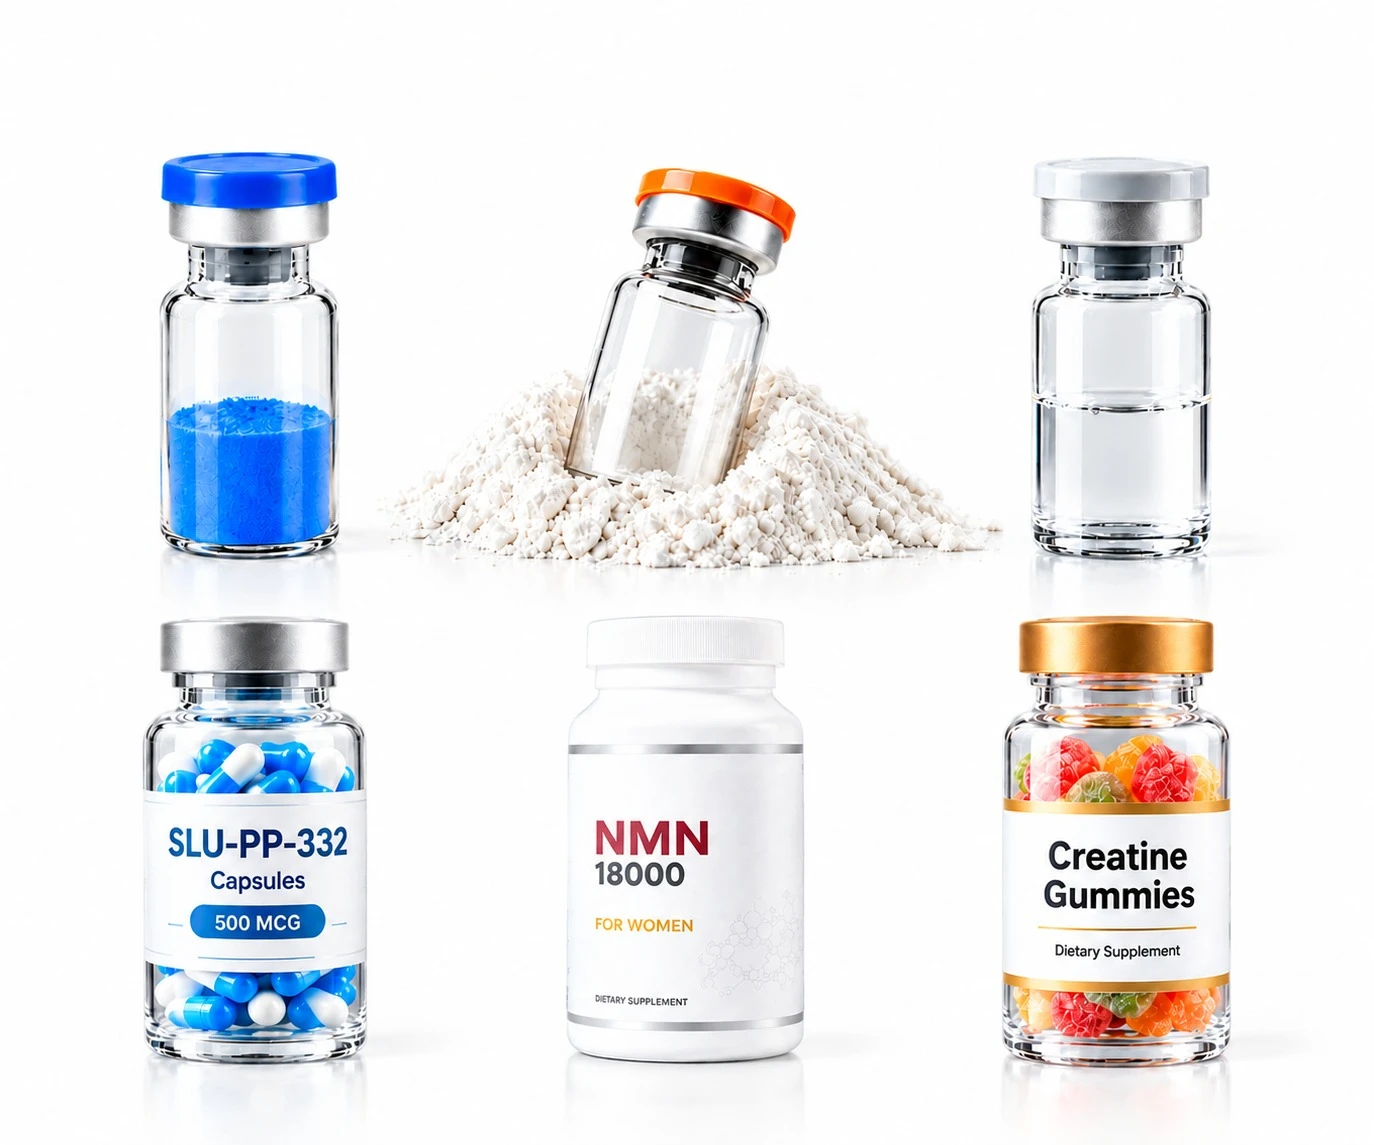
Product Application
For research and development purposes only, including laboratory research, life science studies, cosmetic ingredient development, and early-stage pharmaceutical R&D.
Our Certificate
**ISO 9001 Certified | FDA | GMP-Compliant Facilities | COA Provided with Every Product**
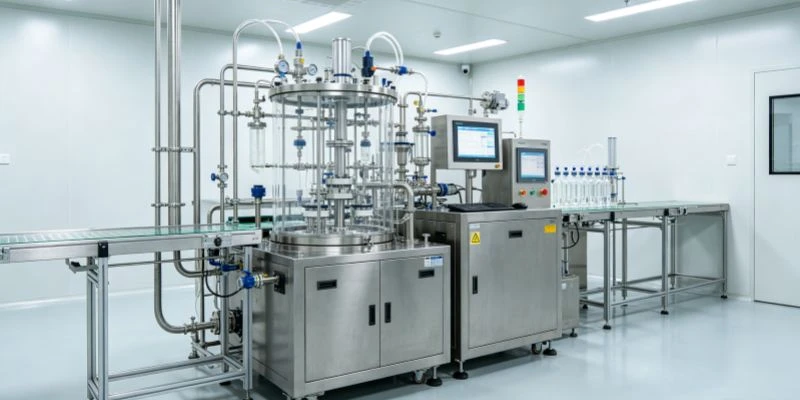
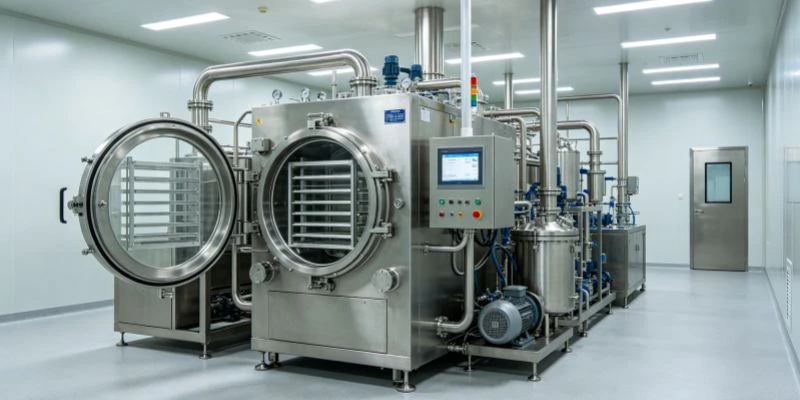
Production Equipment
The plant houses a dedicated quality control center equipped with High-Performance Liquid Chromatography (HPLC) systems, mass spectrometers (MS), moisture analyzers, and microbiological testing equipment.
Why Partner with QHY Bioengineering?
Exceptional Technical Expertise
Our R&D team is led by PhD-level chemistry experts and engineers. With decades of hands-on experience in peptide synthesis, various modifications (phosphorylation, biotinylation, PEGylation, etc.), and purification, we are capable of overcoming complex production challenges.
One-Stop, End-to-End Solutions
We handle the entire production chain in-house-from sequence feasibility analysis, process development, and scale-up production to vacuum lyophilization and final packaging.
Transparent and Traceable Data
We provide a comprehensive data package with every shipment, including the Certificate of Analysis (COA), HPLC purity reports, and MS spectra. All quality control data is clearly presented to the client, ensuring full quality traceability.
Customer-Centric Approach and Long-Term Partnerships
We prioritize building enduring, stable partnerships over one-off transactions. A dedicated project manager oversees your order from start to finish, providing timely responses to all inquiries. Whether addressing routine questions or resolving complex, challenging technical issues, we are fully committed to effective communication and solutions.
Our Vision
We strive to become a globally influential enterprise in the field of green-chemistry peptide manufacturing. By consistently delivering high-quality, cost-effective peptide raw materials, we aim to leverage our production capabilities to drive continuous innovation and progress within the global pharmaceutical and health industries.